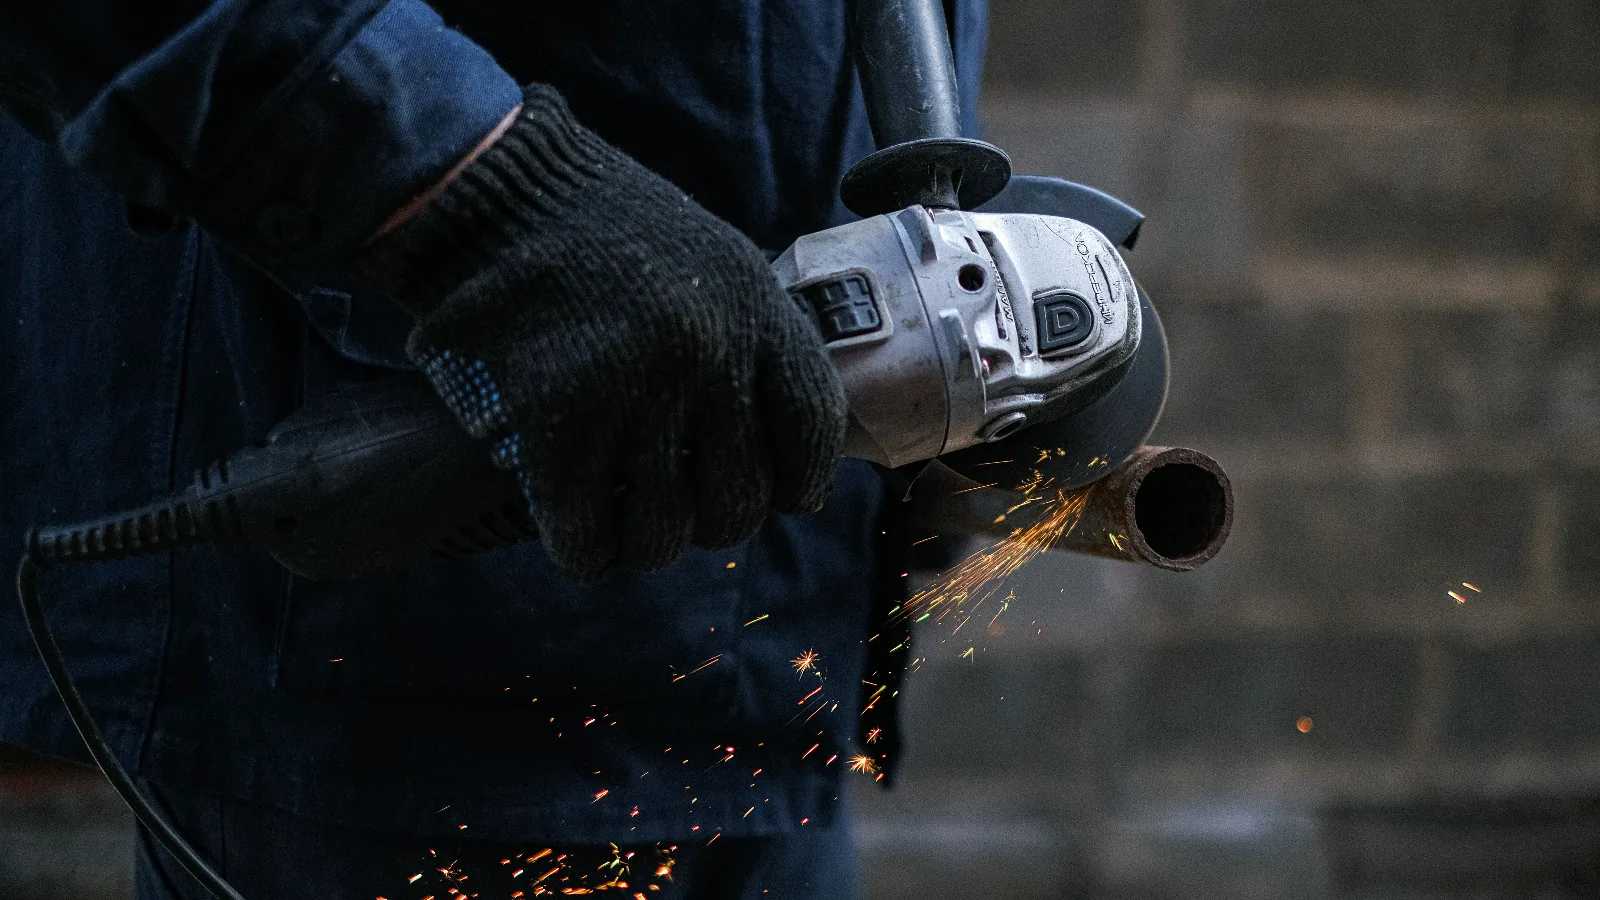
The 6G test is the standard pipe qualification in the Eastern Province: a pipe fixed at 45 degrees, welded without rotating it, so the welder proves flat, vertical and overhead technique in one coupon. AKFAL tests every welder before mobilisation, and most clients test again at the gate.
What is tested
A pipe coupon, usually 6-inch schedule 80 carbon steel, is fixed at 45 degrees. The root pass is welded with TIG (GTAW) and the fill and cap with SMAW, or the whole joint with one process depending on the WPS. Stainless and duplex coupons are used when the job requires them.
How it is judged
The inspector checks the visual first — undercut, porosity, cap profile, root penetration — then sends the coupon for bend tests or radiography. A visually good weld that fails a root bend still fails.
- Root fusion and penetration without excessive suck-back
- No porosity, cracks or slag inclusions
- Undercut within the code limit
- Cap width and reinforcement within tolerance
- Correct interpass cleaning between passes
Common reasons welders fail
Rushing the root, wrong electrode angle in the overhead position, poor interpass cleaning and welding outside the WPS parameters are the usual causes. A welder who works to the WPS card rather than from habit passes more often.
Certificates that help
A 6G certificate from a recognised institute or a previous employer's test record shows you have done it before. An Aramco or SABIC approval means the client can accept you with a shorter re-test. Neither replaces AKFAL's own coupon.
Preparing before you apply
Practise on the position, not the flat. Bring your existing certificates and, if you have them, radiography reports from previous tests. Tell us which processes you are strongest in — a welder honest about being SMAW-only is placed better than one who fails a TIG root.